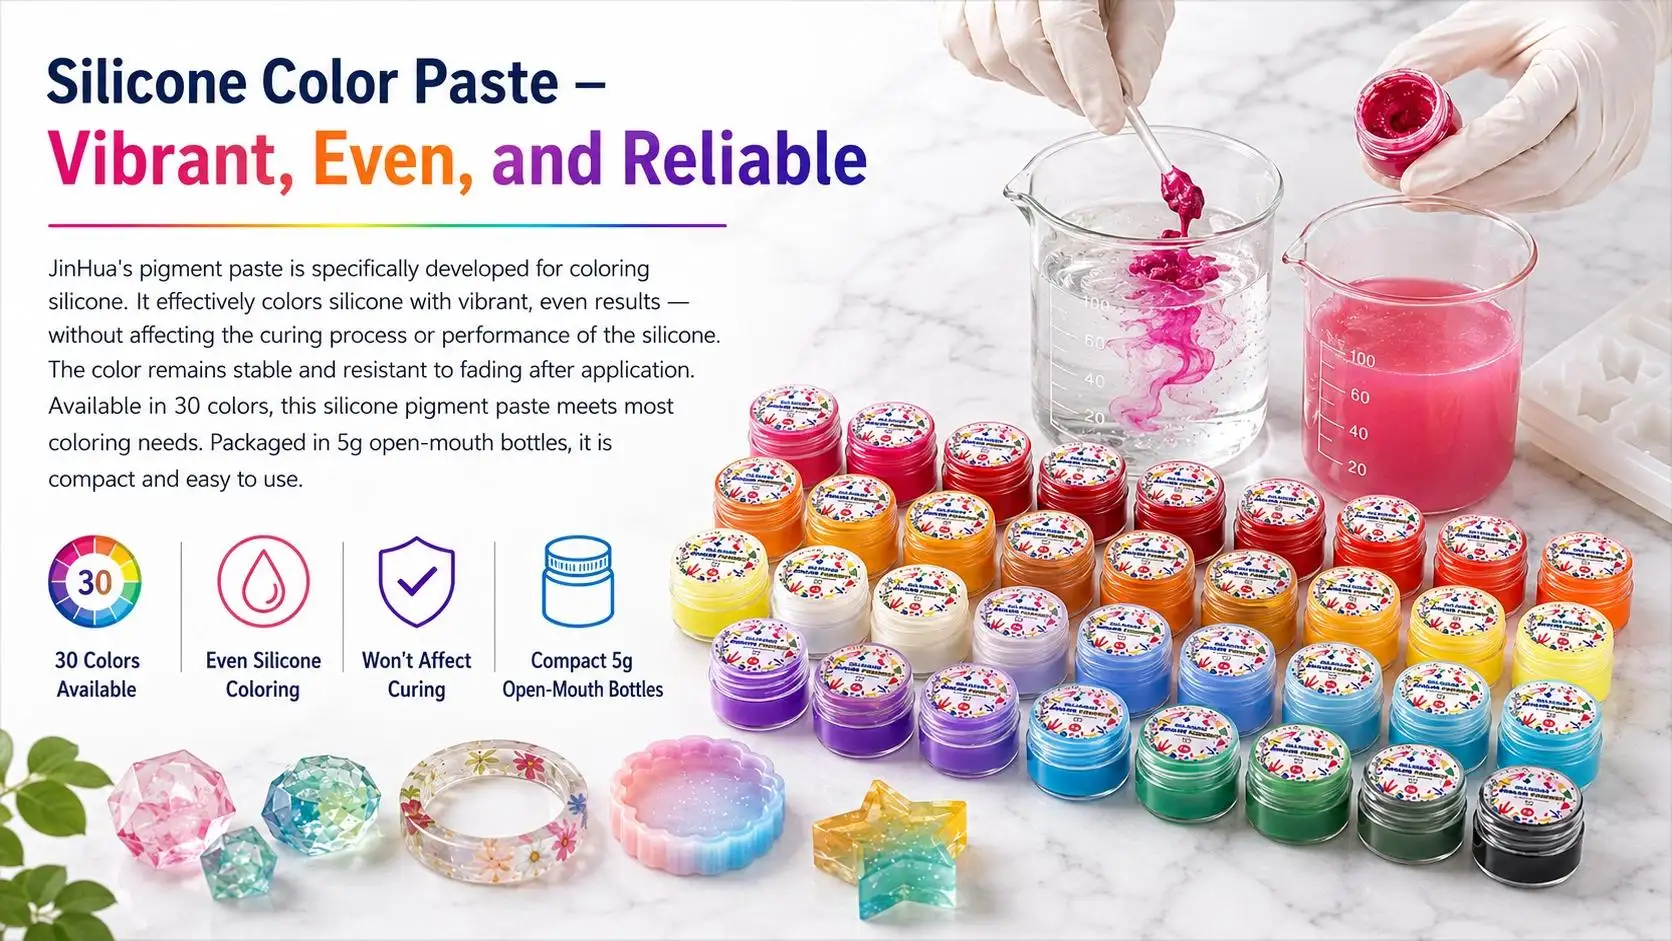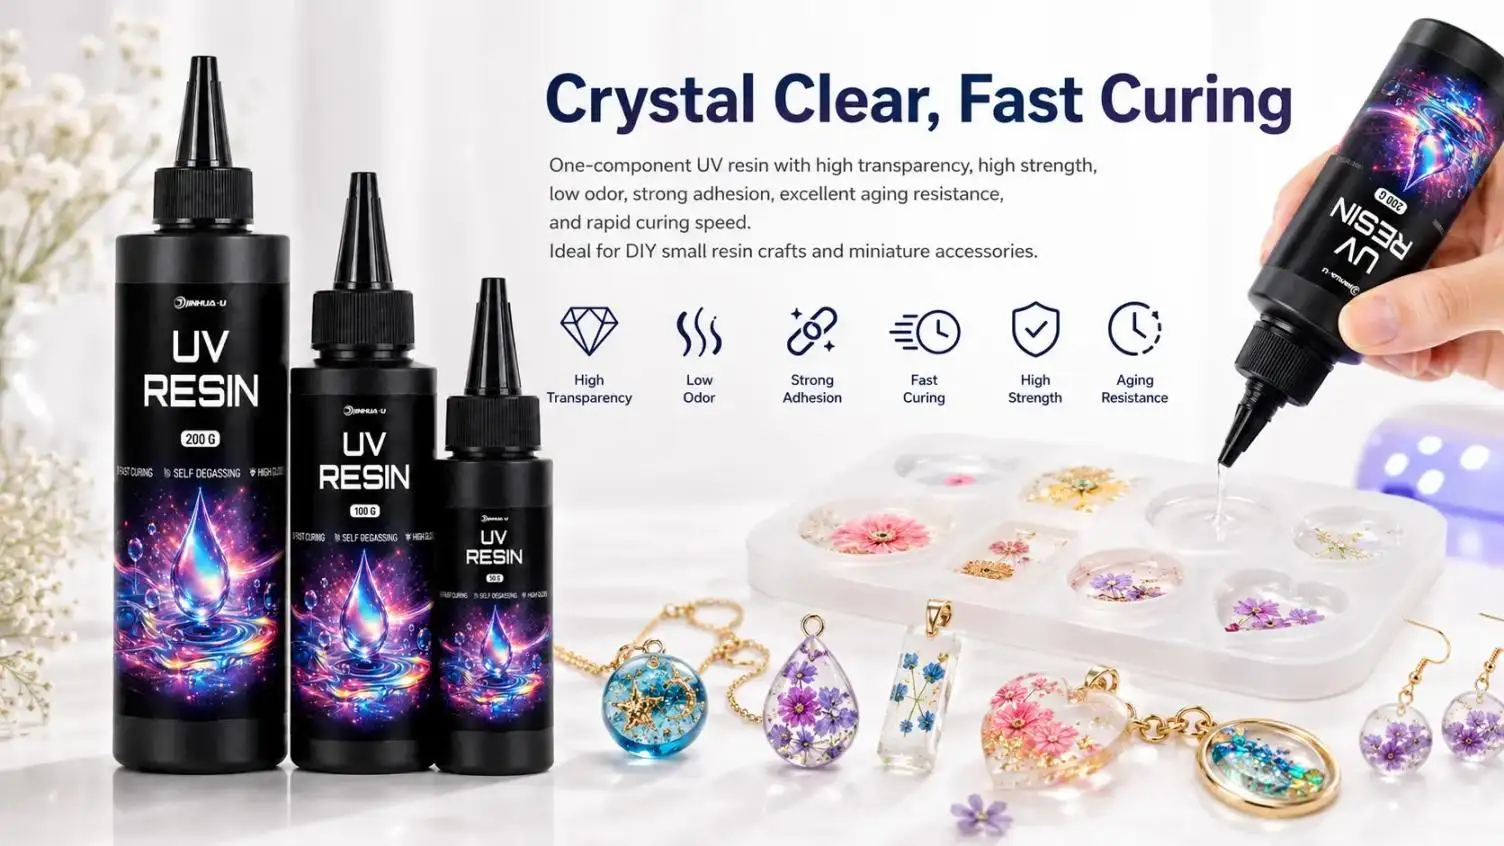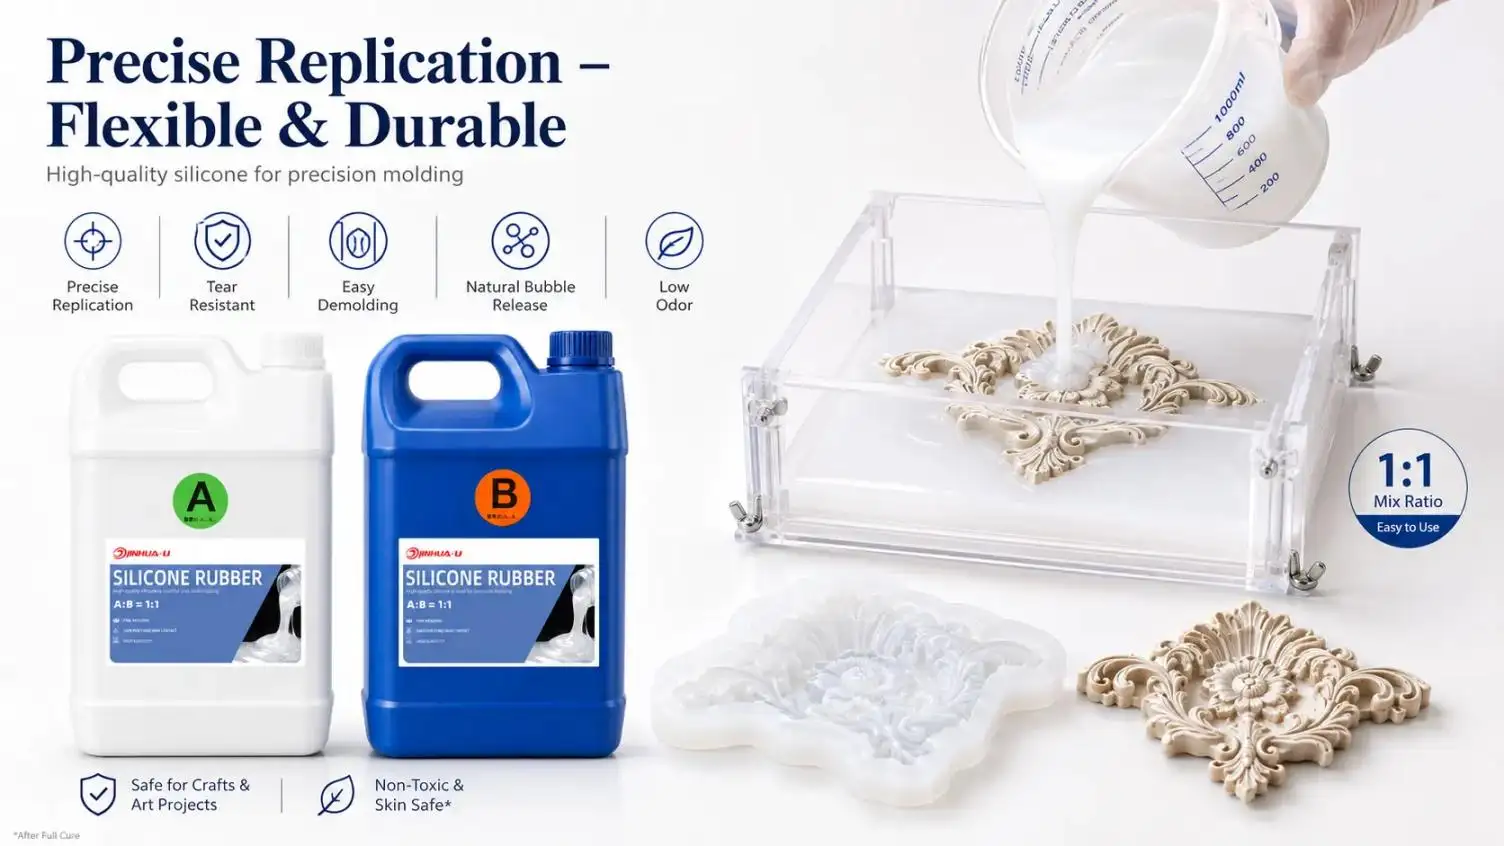


Today, colour is an important factor in the manufacturing process that determines product appearance, brand recognition, performance and the experience of the user. Whether it's plastics, coatings, cosmetics, textiles, construction or industrial uses, manufacturers are looking for high-quality colourants that enable them to produce consistent, attractive and durable coloured products.
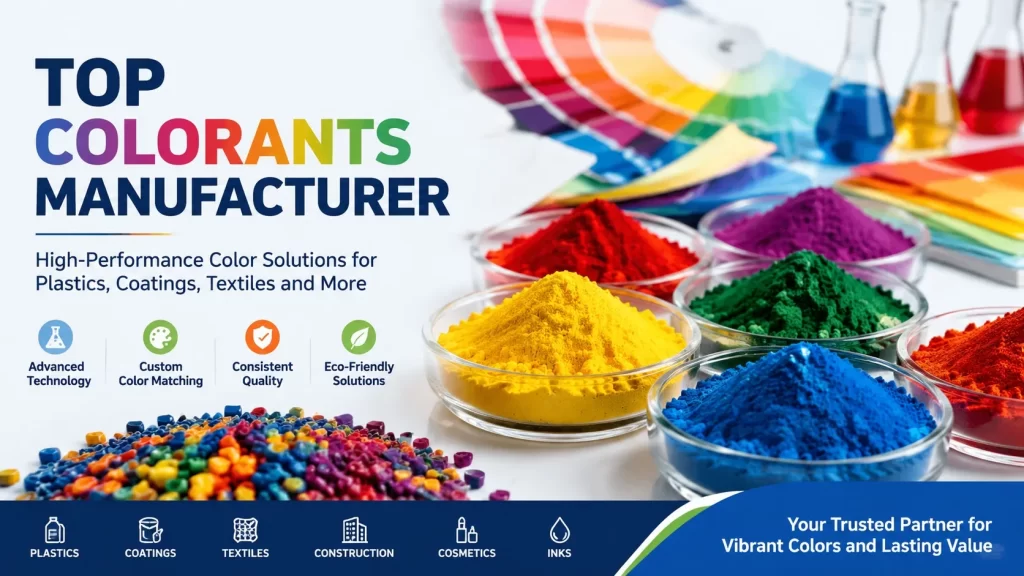
A good manufacturer of colorants has more to offer than just pigments and dyes. High-quality formulation technology, professional technical support and strict quality control are provided by leading suppliers, who offer tailor-made color solutions according to the needs of various industries.
Choosing a reliable top colorants provider is crucial for companies aiming to build their brand success in the long term, and ensuring that the manufacturing capabilities, innovation, and customization services of the partner are also robust.
What Are Colorants?
Colourants are materials, substances or products used for the purpose of imparting colour. These are applied in many industries to achieve a range of desirable effects including visual appeal, added value and functional properties.
There are primarily two types of colorants:
1. Pigments
Pigments are finely divided coloured particles which are suspended in a material. They have good colour fastness, weather resistance and chemical resistance properties.
Pigments are used in many different ways, such as:
- Plastic products
- Automotive coatings
- Building materials
- Inks
- Industrial paints
- Rubber products
Pigments are more desirable for applications where long-lasting color is required.
2. Dyes
Dyes are substances that are soluble and when chemically bonded to the material produce a color. They are typically found in:
- Textiles
- Leather
- Paper
- Food packaging
- Cosmetics
Typically dyes can supply colorful and vibrant hues that have strong coloring power.
Pigment and dye solutions are available from a professional colourants manufacturer, depending on the specific requirements of the application.
Why Choose a Professional Colorants Manufacturer?
Product quality, production efficiency and competitiveness are directly influenced by the choice of the manufacturer. A professional colorants supplier has some significant benefits.
1. Customized Color Solutions
Color needs vary from industry to industry. A leading manufacturer can make a custom formulation based on the following:
- Color specifications
- Material compatibility
- Processing conditions
- Environmental requirements
- Performance expectations
If customers have special shades, durability or application properties their experienced colorants manufacturers can offer them solutions accordingly.
2. Consistent Product Quality
Maintaining color consistency is very important for mass production. The professional suppliers adopt advanced testing equipment and strict quality management systems to guarantee that every batch can meet customers' requirement.
Common quality control elements are:
- Color matching analysis
- Particle size testing
- Heat resistance testing
- Chemical stability testing
- Dispersion performance evaluation
Consistency in quality allows manufacturers to minimize production problems and ensure consistency of their brand.
3. Advanced Manufacturing Technology
An advanced production technology is being invested by a leading manufacturer of colourants to enhance production efficiency and product performance.
Advanced Manufacturing processes:
- Precision pigment dispersion
- Advanced grinding technology
- Automated production systems
- Laboratory color matching equipment
- Quality inspection procedures
Through these technologies, manufacturers can develop colorants that are very stable, concentrated and performing in a consistent manner.
Applications of Colorants Across Industries
Colorants are essential materials used in many industries worldwide.
Plastic Industry
Plastic manufacturers rely on colorants to create attractive and functional products, including:
- Packaging materials
- Consumer electronics
- Household products
- Automotive components
- Plastic films
High-performance plastic colorants offer excellent heat resistance, migration resistance, and compatibility with different polymers.
Coatings and Paint Industry
Colorants are widely used in decorative and protective coatings.
Applications include:
- Architectural paints
- Industrial coatings
- Powder coatings
- Automotive finishes
High-quality colorants improve appearance while maintaining durability against sunlight, weather, and chemicals.
Textile Industry
Textile manufacturers require colorants that provide:
- Bright colors
- High washing resistance
- UV stability
- Long-lasting appearance
Professional dye and pigment suppliers support textile producers with reliable color solutions.
Construction Materials
Colorants enhance the appearance of construction products such as:
- Concrete
- Tiles
- Flooring materials
- Decorative surfaces
Durable construction colorants help maintain attractive appearances in outdoor and indoor environments.
Cosmetics and Personal Care
The cosmetics industry requires safe and high-performance colorants for:
- Makeup products
- Skincare products
- Personal care items
Manufacturers must provide colorants that meet strict safety and regulatory standards.
Key Factors When Selecting a Colorants Manufacturer
Choosing the right supplier requires careful evaluation. Businesses should consider the following factors:
1. Product Range
A reliable manufacturer should offer a wide selection of colorants, including:
- Organic pigments
- Inorganic pigments
- Dye solutions
- Masterbatch colorants
- Custom color formulations
A broad product portfolio allows customers to find suitable solutions for different applications.
2. Customization Capability
Different industries require different color performance. The best colorants manufacturers provide OEM and ODM services, including:
- Custom color matching
- Formula adjustment
- Application testing
- Packaging customization
Customization helps businesses create unique products and improve market competitiveness.
3. Quality Certifications
Professional manufacturers follow international quality standards to ensure product safety and reliability.
Important certifications may include:
- ISO quality management systems
- Environmental compliance
- Industry-specific safety standards
Certified suppliers provide greater confidence for global customers.
4. Technical Support
Color development can involve complex technical challenges. Experienced manufacturers provide professional support, including:
- Material compatibility guidance
- Processing recommendations
- Color optimization
- Problem-solving assistance
Strong technical service helps customers achieve better production results.
Benefits of Working With a Global Colorants Manufacturer
Partnering with an experienced manufacturer provides several business advantages:
Improved Product Appearance
High-quality colorants create attractive products that increase customer appeal and brand value.
Better Production Efficiency
Reliable colorants reduce production problems caused by inconsistent color or poor dispersion.
Cost Optimization
Professional suppliers help customers select suitable formulations to reduce waste and improve manufacturing efficiency.
Faster Product Development
Customized color solutions allow companies to launch new products faster and respond quickly to market trends.
Future Trends in the Colorants Industry
The colorants industry continues to evolve with changing market demands. Several trends are shaping future development.
Eco-Friendly Colorants
Environmental protection has become a major focus. Manufacturers are developing:
- Low-impact pigments
- Sustainable dyes
- Non-toxic formulations
- Environmentally friendly solutions
Green color technologies help industries meet sustainability goals.
High-Performance Color Solutions
Modern applications require colorants with improved performance, including:
- Higher temperature resistance
- Better UV stability
- Enhanced chemical resistance
- Improved durability
Advanced formulations are becoming increasingly important in automotive, electronics, and industrial markets.
Digital Color Management
Digital technology is improving color development through:
- Computerized color matching
- Automated testing systems
- Digital formulation databases
These innovations help manufacturers achieve faster and more accurate color solutions.
Why Choose Us as Your Trusted Colorants Manufacturer?
We are a professional colorants manufacturer, which is committed to providing customers with reliable, customized and high quality color products all over the world.
Our advantages include:
- Advanced production facilities
- Strict quality control systems
- Professional color matching services
- Customized OEM and ODM solutions
- Competitive manufacturing capabilities
- Experienced technical support team
From colorants for plastics, coatings, textiles, construction materials to specialty applications, we have the solutions to fit your needs.
Conclusion
In the end, selecting the right top colorants manufacturer is crucial for businesses looking to maintain consistent quality, tailor solutions to their specific needs, and foster long-term partnerships. Colorants are used in various industries for a variety of applications to enhance the appearance, performance and competitiveness of products and various applications.
Using advanced technology, robust research and service for customers, professional colorants manufacturers enable companies to get consistent colors and develop improved products, which could be sold in worldwide markets.
Working with an experienced colorants manufacturer can help you to achieve the quality, flexibility and innovation you need for future growth if you are looking for a reliable partner to produce customized color solutions.